About food-grade mesh conveyor
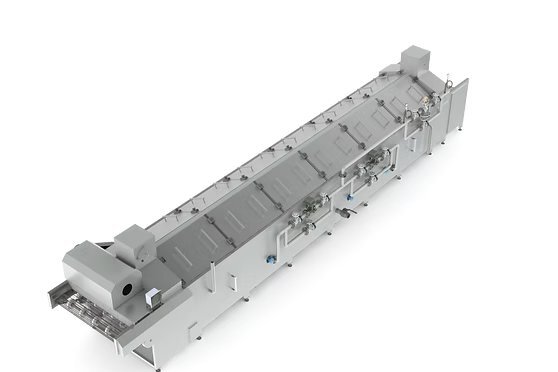
Discover the top-rated Food-Grade Mesh Conveyor-an indispensable solution for food processing, packaging, and transfer applications. Engineered with a robust stainless steel (SS304/SS316) welded or bolted frame, it ensures remarkable hygiene and pivots seamlessly into HACCP environments. Highlighted by unbeatable price, customizable belt width (300mm to 1000mm), and a ravishing open wire mesh design, it offers rapid cleaning and corrosion resistance. With customizable capacity, PLC optional control, and noise levels below 70 dB(A), this modular conveyor delivers pivotal reliability for your facility. Warranty extensions available!
Exceptional Application Versatility in Food Plants
Our food-grade mesh conveyor is tailored for a remarkable range of applications, from bakery and confectionery lines to dairy, meat processing, and packaging plants. Designed for continuous indoor operation, it is ideally suited for plant environments where hygienic material transfer, efficient sorting, and sanitary handling are pivotal. Usage versatility and modular design make it an excellent choice for both high-volume production and flexible, specialty food processing tasks throughout the industry.
Premium Access, Delivery Timelines & Proposal Outlay
Sample units of the food-grade mesh conveyor are available for demonstration, exemplifying our premium manufacturing standards. Delivery time typically ranges from two to six weeks following order confirmation, depending on customization needs. FOB Port options can include major Indian ports per proposal discussion. Transparent proposal amounts and efficient outlay estimates ensure seamless acquisition and rapid integration, helping clients optimize investment returns with reliable supplier support.
FAQ's of food-grade mesh conveyor:
Q: How is the mesh conveyor cleaned for sanitation in food environments?
A: The conveyor is specially designed for easy access and rapid cleaning, enabling thorough sanitation routines required in HACCP-compliant environments. Its open wire mesh and modular construction help reach critical areas efficiently.
Q: What applications is the mesh conveyor suitable for?
A: This conveyor is ideal for material handling within food processing, packaging, and transfer operations in both large-scale industrial plants and specialized food production facilities.
Q: When can I expect delivery after placing an order?
A: Standard delivery ranges from two to six weeks, depending on customization and production schedules. Expedited or prioritized shipping can be discussed during the proposal phase.
Q: Where can the mesh conveyor be installed?
A: It is designed for indoor, floor-mounted installation-making it well-suited for production halls, food plants, and packaging areas.
Q: What distinguishes the conveyor's usage and benefit?
A: The conveyor stands out for its hygienic operation, corrosion resistance, customizable capacity, and quick cleaning attributes, ensuring efficient and reliable material handling in strict food industry environments.
Q: How customizable are the conveyor specifications?
A: Almost every aspect, including belt width, conveying length, frame configuration, and accessory selection, can be tailored to meet particular operational needs. Capacity and power adjustments are available as well.




 Send Inquiry


 Send Inquiry
